Petroleum Coke Grinding & Processing Solutions
Petroleum Coke Powder for Lime Kilns
2026-10-25 13:33:29
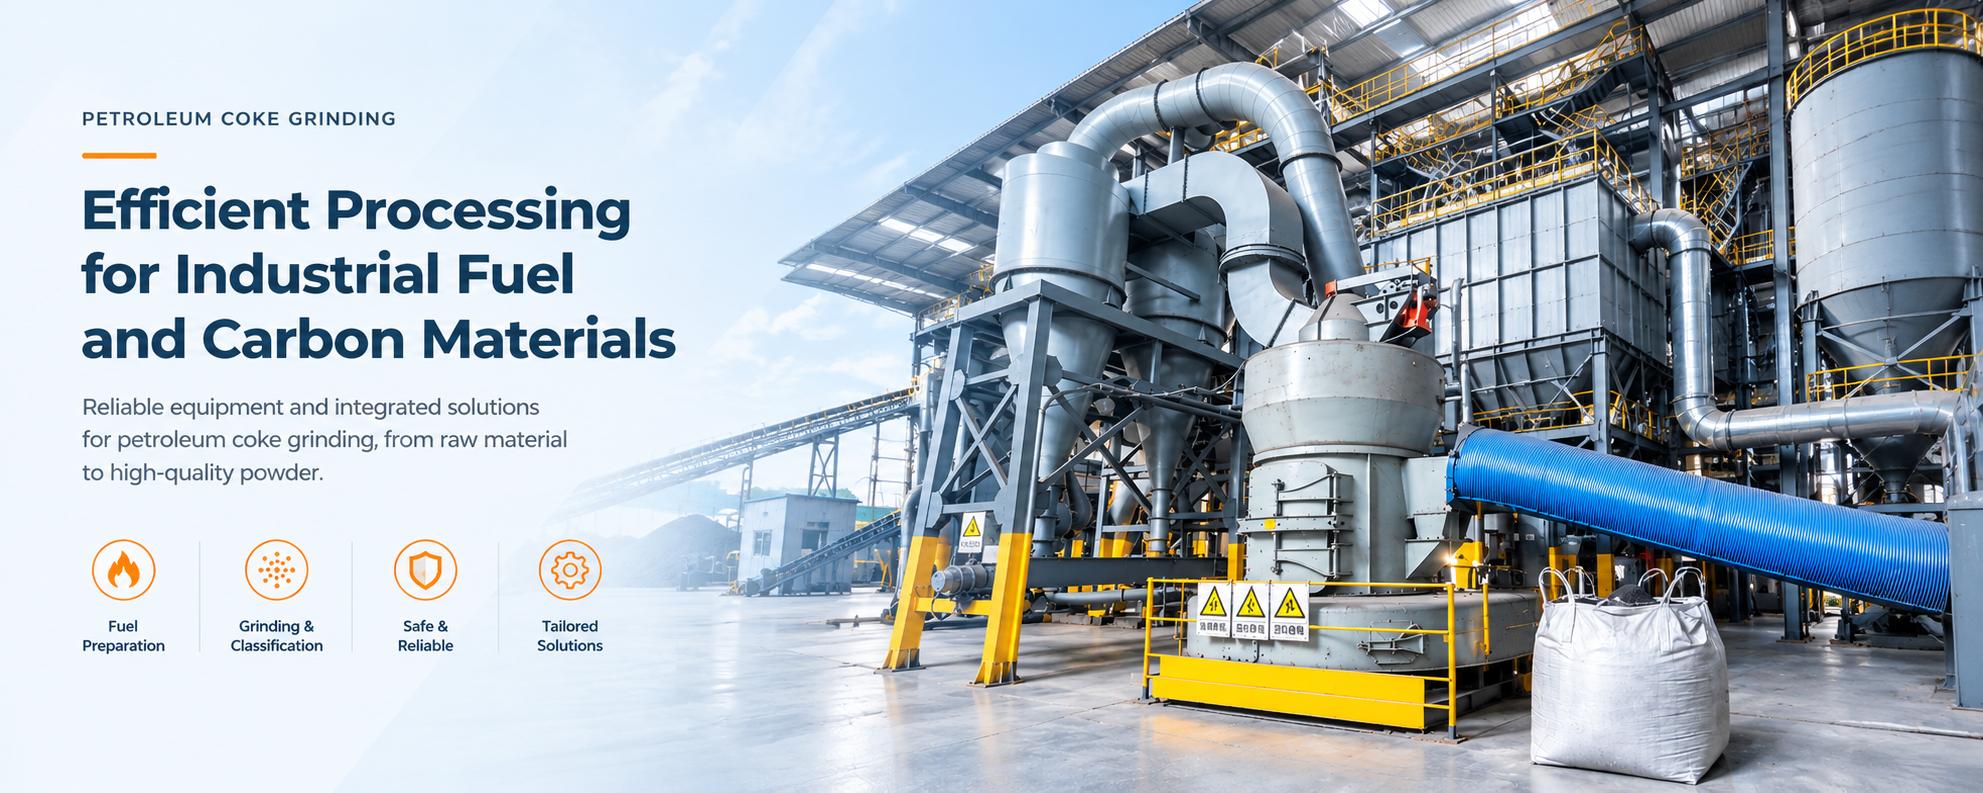
Petroleum coke powder can replace part of the conventional fuel used in suitably designed lime kilns. Its practical value depends on more than heating value: the kiln must burn the powder reliably while maintaining lime quality, production capacity, and emissions compliance. Sulfur and metals in the fuel are particularly important because they can affect both the product and kiln operation.
The key requirement is compatibility—between the petroleum coke, the combustion system, and the required lime specification. A fuel acceptable for one lime plant may be unsuitable for another producing a different product or using a different kiln design.
First Identify the Lime Kiln Application
“Lime kiln” covers more than one industrial duty. Commercial lime plants calcine limestone or dolomitic stone, while kraft pulp mills use lime recovery kilns to regenerate lime from lime mud. Both applications may consider petroleum coke, but their feed materials, product requirements, and process constraints differ.
| Application | Main Evaluation Priority | Important Qualification |
|---|---|---|
| Rotary kiln producing commercial lime | Combustion performance, product sulfur, lime reactivity, and output | Fuel flexibility does not remove the need to meet the customer’s lime specification |
| Vertical kiln producing commercial lime | Compatibility with the specific kiln and fuel-injection arrangement | Suitability cannot be inferred from a rotary-kiln installation |
| Lime recovery kiln in a kraft pulp mill | Available lime, sulfur and metals inputs, kiln deposits, and recovery-cycle effects | Fuel changes must be assessed as part of the mill’s wider chemical balance |
Commercial lime technology selection depends on the intended market, lime reactivity, sulfur limits, fuel properties, and operating costs. Recovery-kiln experience adds separate concerns about available lime and chemical recovery. These requirements should not be combined into a single universal fuel specification.
Why Fine Grinding Matters for Petroleum Coke Combustion
Petroleum coke has relatively low volatile matter, making ignition and stable combustion more demanding than with readily ignitable fuels. Lime recovery kiln guidance identifies it as a difficult fuel to burn and describes co-firing with gas or oil to support flame stability. The required support-fuel share is an operating decision, not a fixed value applicable to every kiln.
Pulverizing the coke prepares it for controlled solid-fuel firing. However, grinding alone cannot compensate for inadequate fuel-air mixing, unsuitable burner geometry, or insufficient combustion time. Solid-fuel burner design and fuel delivery must be evaluated together with powder preparation.
Do Not Specify the Powder by Mesh Number Alone
For a grinding project, define the finished powder using an agreed test method and measurable acceptance limits. The specification should state:
The selected sieve opening or particle-size measurement method.
The permitted residue or particle-size distribution.
Any separate limit on oversized particles.
The required moisture at the agreed sampling point.
The throughput at which these requirements must be maintained.
Have the kiln and burner teams approve this specification before final equipment selection. Avoid copying a fineness target from a cement plant or a different lime kiln without confirming the actual combustion duty.
Sulfur Can Affect Lime Quality as Well as Emissions
A lime kiln contains calcium-rich material that can absorb sulfur from combustion gases. This does not make sulfur irrelevant: absorption can form calcium sulfate, changing the material leaving the kiln and reducing available lime in recovery-kiln applications. Sulfur behavior also depends on total input and operating conditions.
Commercial Lime: Start with the Product Limit
For merchant lime, the acceptable fuel depends partly on the customer’s sulfur specification. Lime-kiln technology guidance identifies product sulfur as an important selection criterion and notes restrictions on high-sulfur fuels for certain steel-industry customers. The permitted fuel should therefore be established from the required product, not simply from the kiln’s ability to burn it.
Recovery Lime: Evaluate the Wider Process
In kraft recovery applications, sulfur-containing fuels can affect available lime, ring formation, sulfur dioxide emissions, and the mill’s sulfur balance. These consequences must be included when comparing petroleum coke with gas or fuel oil. Lower fuel expenditure may be offset by additional make-up lime or other operating costs.
Do Not Assume Complete Sulfur Capture
Sulfur absorption is not an unlimited control mechanism. Recovery-kiln research shows that absorption efficiency can decrease as sulfur input increases, allowing more sulfur dioxide to leave the kiln. Product testing and emissions assessment are both necessary; one cannot replace the other.
Metals and Deposits Need Separate Attention
Petroleum coke can introduce metals, including vanadium, that deserve specific review. Recovery-kiln operating guidance identifies sulfur and vanadium contamination as limitations on successful petroleum coke use. The fuel certificate should therefore include relevant metals rather than report only moisture, ash, sulfur, and heating value.
Deposit formation also requires a plant-specific assessment. High-sulfur fuel use can contribute to ring hardening in recovery kilns, but fuel chemistry is not the only operating variable. Monitor the kiln’s behavior during trials instead of assuming that an acceptable laboratory analysis guarantees deposit-free operation.
Defining a Liming Heavy Industry Grinding Project
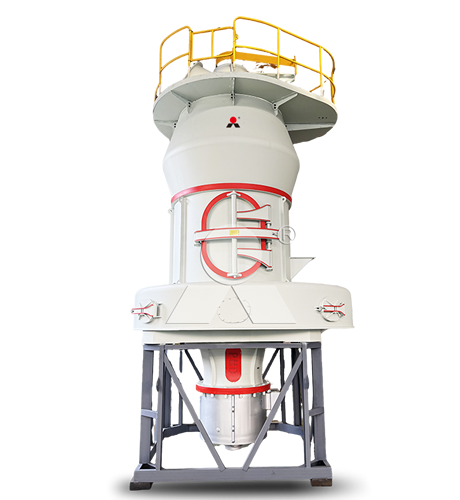
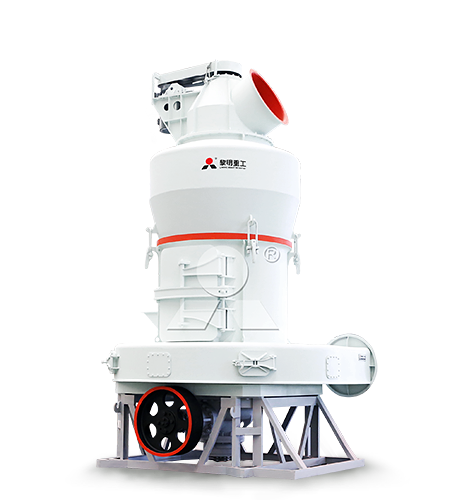
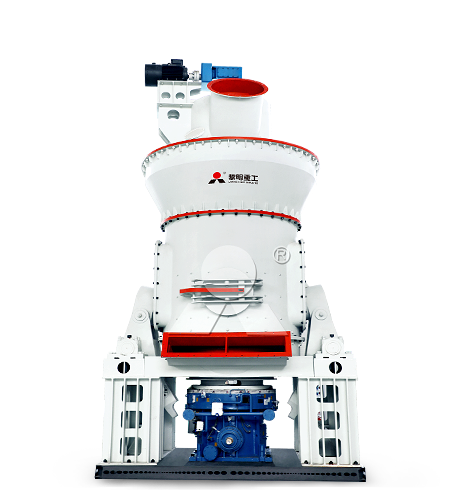
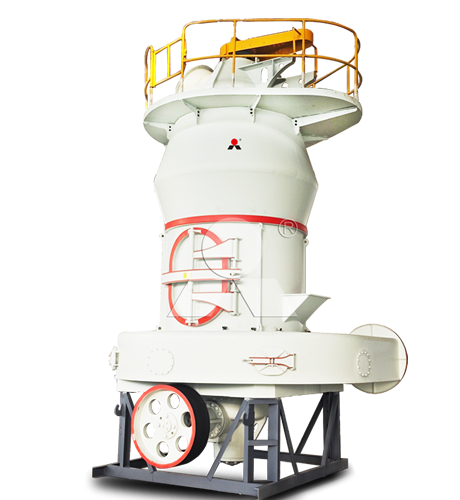
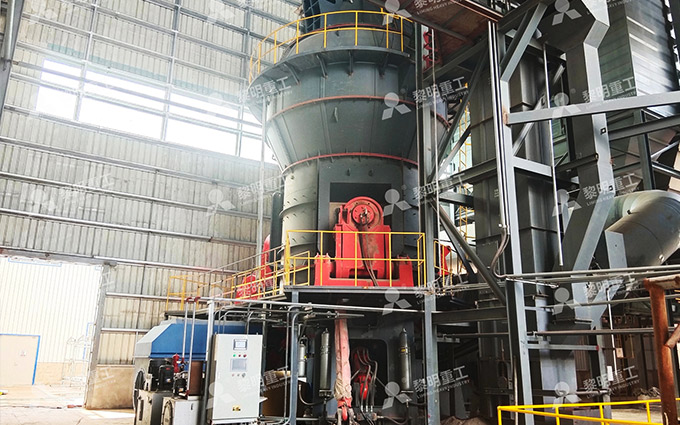
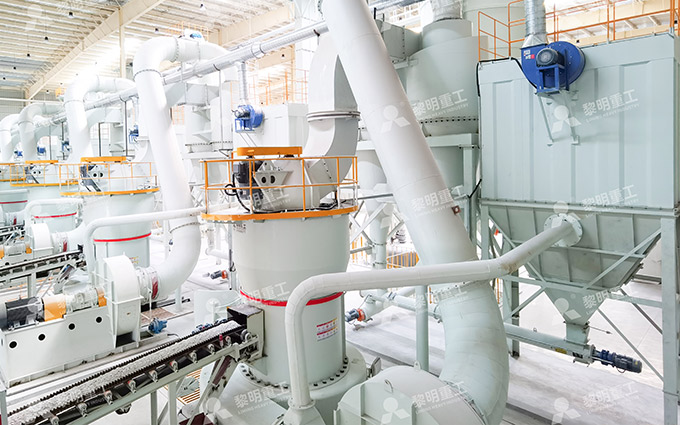
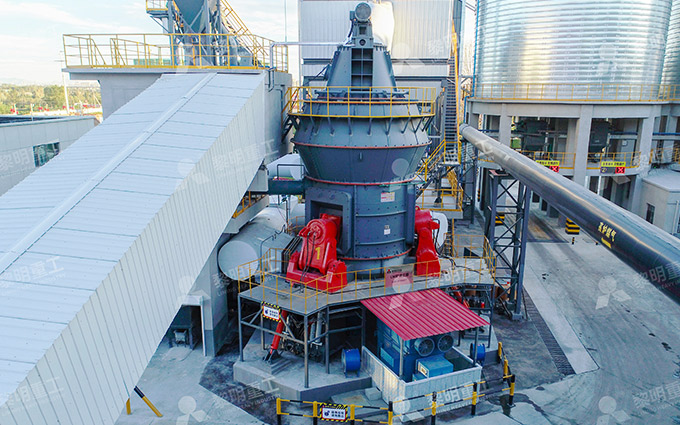
For a petroleum coke powder preparation project, evaluate a Liming Heavy Industry grinding system against the actual feed and kiln-approved powder specification. Mill selection should follow material testing and duty definition—not a nominal capacity figure copied from another installation.
The technical inquiry should include:
Material condition: confirm whether the feed is green petroleum coke, calcined coke, or a specified blend.
Fuel analysis: provide moisture, volatile matter, ash, sulfur, heating value, and relevant metals, with reporting bases stated.
Incoming feed: identify maximum lump size, normal size distribution, and expected moisture variation.
Finished powder: state fineness, coarse-particle limits, moisture requirements, and test methods.
Production duty: define normal and peak throughput, operating hours, and required storage capacity.
Plant interfaces: identify available drying heat, layout constraints, and the boundary between grinding, storage, dosing, and burner delivery.
Ask for performance commitments tied to these conditions. A meaningful acceptance test measures powder quality and production rate together using representative petroleum coke.
Keep Grinding Capacity Separate from Burner Delivery
The grinding plant prepares fuel; the dosing and conveying system delivers it to the flame. Both duties need defined performance requirements. Solid-fuel combustion engineering treats burner design and fuel delivery as connected parts of kiln performance.
During project planning, establish who is responsible for each interface:
Discharge from the grinding and collection system.
Transfer to the powder storage silo.
Extraction and controlled fuel metering.
Delivery to each firing point.
Coordination with support fuel and kiln operating controls.
Include a site-specific combustible-dust and fire-risk assessment in the engineering scope. The applicable protective measures should be defined by qualified specialists for the actual material, equipment arrangement, and local requirements rather than copied from an unrelated powder plant.
Use a Controlled Trial Before Increasing the Fuel Share
A phased trial provides a clearer basis for deciding whether petroleum coke is suitable than a fuel-price comparison alone. Recovery-kiln guidance shows that both combustion behavior and contamination can limit practical use.
Agree the trial’s acceptance criteria in advance. Track:
Powder fineness, moisture, and fuel-delivery consistency.
Flame stability and support-fuel consumption.
Kiln output and specific heat consumption.
Product sulfur and the required lime-quality properties.
Deposit development and operating interruptions.
Emissions against the applicable permit limits.
For recovery kilns, available lime and relevant recovery-cycle changes.
Increase petroleum coke use only within the limits demonstrated by the trial. The appropriate replacement level is the one that preserves the required product and stable operation—not the highest percentage the fuel system can physically deliver.
Evaluate the Cost per Ton of Acceptable Lime
The economic comparison should include delivered fuel cost, grinding electricity, drying requirements, support fuel, maintenance, and any changes in kiln output or product acceptance. In recovery applications, include the potential effect on make-up lime requirements, which is a recognized consequence of sulfur and metals inputs.
A sound petroleum coke project begins with the lime specification and kiln constraints, then works backward to fuel quality, powder preparation, and equipment selection. This keeps the investment focused on producing acceptable lime reliably rather than achieving a lower fuel purchase price in isolation.